Plate and Sheet Laser Cutting in Southern California
Flat plate and sheet laser cutting in Fontana, California, in steel, aluminum and stainless on two 3 kW fiber lasers, with waterjet available for thick material that exceeds the laser envelope.
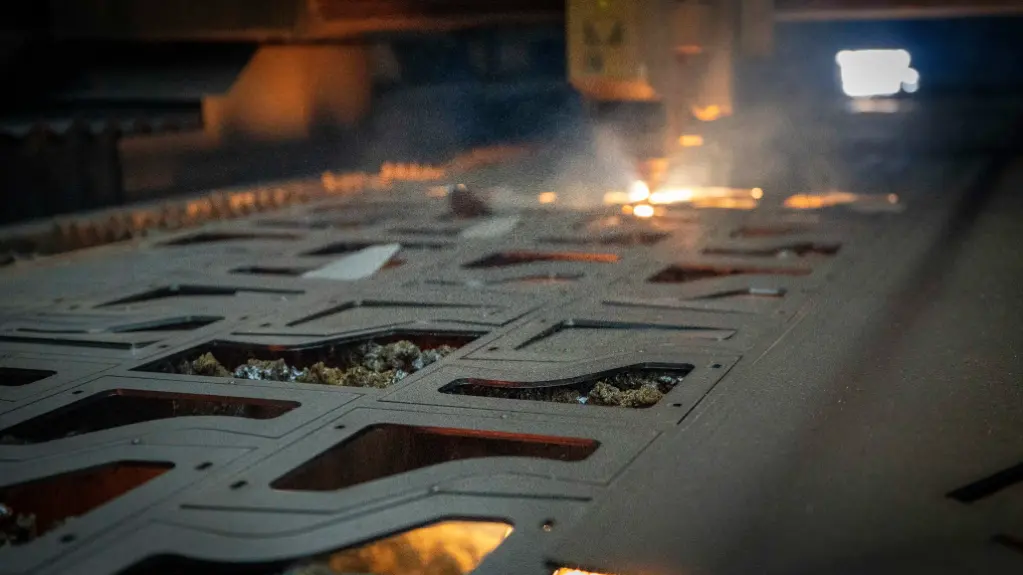
Plate cutting capacity
| Machines | 2 × 3 kW fiber lasers |
| Bed size | 76 in x 150 in |
| Sheet stock | 48 x 120 in standard; 60 x 120, 72 x 120 and 96 x 240 in for oversize parts |
| Mild steel grade by thickness | A1008 CR to 0.125 in; A1011 P&O to 0.375 in; A36 HR above |
| Laser — steel | Up to 0.75 in thick |
| Laser — aluminum | Up to 0.25 in thick |
| Laser — stainless | Up to 0.25 in thick |
| Waterjet — steel | Up to 4.00 in thick |
| Waterjet — aluminum | Up to 8.00 in thick |
| Waterjet — stainless | Up to 3.00 in thick |
| CAD formats accepted | SolidWorks (.sldprt), Parasolid (.x_t), STEP, IGES |
| Lead time | Quoted with every job |
Tolerances
| Feature tolerance | ±0.005 in |
| Overall part tolerance | ±0.015 in |
Tighter tolerances available on request.
Plate laser cutting gives clean, smooth edges that are effectively ready to weld. Compared with waterjet or plasma, there is far less cleanup and far less time lost to secondary operations before the part moves to forming.
Holes, alignment keys and custom profiles are cut in the same pass, which cuts assembly time and improves accuracy downstream. For material thicker than the laser envelope we run waterjet — steel to 4 in, aluminum to 8 in and stainless to 3 in.
Two 3 kW fiber lasers with 76 × 150 in beds cut steel, stainless and aluminum. Standard plate stock is 48 × 120 in, stepping up to 60 × 120, 72 × 120 or 96 × 240 in for oversize parts. Mild steel is cut from the grade that suits the thickness: A1008 cold rolled up to 0.125 in, A1011 pickled and oiled over 0.125 to 0.375 in, and A36 hot rolled above that.
Flat parts are nested and quoted by the sheet, and nesting happens only within the file you upload, so send all the parts of one material as a single multibody file: they share stock and setups. Parts uploaded one at a time each get their own sheet and setup and price high. A DXF alone cannot be quoted because it carries no thickness; extrude it to your plate thickness and save it as a part first. Press brake forming runs in the same building, so cut-and-form jobs are quoted as one.
From Fontana we cut plate for fabricators and OEMs across San Bernardino and Riverside counties, Los Angeles and Orange County, and ship across Southern California. ITAR or export-controlled files should not go through the instant quote; email them to sales@calwestmfg.com.
Common questions
What plate thickness can you laser cut?
On the laser: steel up to 0.75 inch, aluminum and stainless up to 0.25 inch. Thicker material runs on the waterjet: steel to 4 inches, aluminum to 8 inches and stainless to 3 inches.
How much edge cleanup is needed before welding?
Very little. Laser-cut edges come off clean and smooth and are effectively ready to weld, with far less cleanup than waterjet or plasma before the part moves to forming.
Can holes and alignment features be cut in the same pass?
Yes. Holes, alignment keys, part numbers and custom profiles are cut in the same pass as the outline, which removes layout and drilling from the build and improves accuracy downstream.
What should I send for a plate laser quote?
A 3D model in SolidWorks (.sldprt), Parasolid (.x_t), STEP or IGES, with material and finish requirements called out so nothing stalls in planning. A DXF alone cannot be quoted because it has no thickness; extrude it to the plate thickness and save it as a part.
How should I send a job with many flat parts?
In one multibody file per material. Flat parts nest only within the file they arrive in and are quoted by the sheet, so all the steel in one file and all the aluminum in another gives the lowest price. Parts sent one at a time each get their own sheet and setup.
What grade of mild steel do you cut?
It follows the thickness: A1008 cold rolled up to 0.125 inch, A1011 pickled and oiled over 0.125 to 0.375 inch, and A36 hot rolled above 0.375 inch. Call out a different grade on the drawing if your part needs one.
Where is the plate laser and who do you serve?
Fontana, California, in the Inland Empire. We cut plate for customers across San Bernardino and Riverside counties, Los Angeles and Orange County, and ship across Southern California.
Before you send a file
- K-factor and bend radius chart
- Press brake forming
- Sheet metal in SolidWorks
- Machine capacity and max sizes
Other services
- Tube Laser Cutting
- CNC Tube Bending
- Press Brake Forming
- Welding
- CNC Machining
- Weldments
- Robotic Integration
- All services
Design guides and reference
- Tube bend radius chart (CLR)
- Tube bending design rules
- Plate stock sizes and steel grades
- How our instant quote prices a job
- Tubing in SolidWorks video course
- All design guides
- Quality and AS9100D certification
- Case studies
- Contact us
Get a quote on plate laser cutting
Call out material and finish requirements with your file so nothing stalls in planning.
Request a quote →